
 By Mr.Sun
A handheld analyzer reports a familiar alloy name, and the shipment appears ready for release. The remaining question is whether that instrument has actually measured the element that distinguishes the ordered grade. For carbon-dependent requirements, a confident grade label on an XRF screen can be insufficient evidence.
Positive material identification is most useful when the verification plan starts with the required elements and possible mix-ups. It becomes less useful when every available instrument is treated as interchangeable. Casting buyers should agree what the test is intended to establish before specifying a universal PMI instruction.
Separate alloy sorting from full grade verification
Portable X-ray fluorescence can be effective for checking many alloying elements and identifying material mix-ups. However, conventional handheld XRF does not directly measure carbon. Evident’s technical guidance identifies this limitation among the considerations for PMI. A low-carbon designation therefore needs a suitable analytical method rather than an inference from chromium and nickel alone.
Optical emission spectroscopy can measure carbon when the instrument, calibration and sample preparation support that purpose. This does not mean every OES configuration is automatically suitable for every alloy. The laboratory still needs an appropriate method, reference materials and reporting capability for the required range.
Compare the evidence rather than the equipment name
An order for cast stainless components may require both a heat analysis and a check against accidental mixing after machining. Those are related but different tasks. A traceable laboratory result can support the material specification, while a portable check can provide an additional identity control at a later stage.
| Verification need | Handheld XRF | Suitable OES analysis |
|---|---|---|
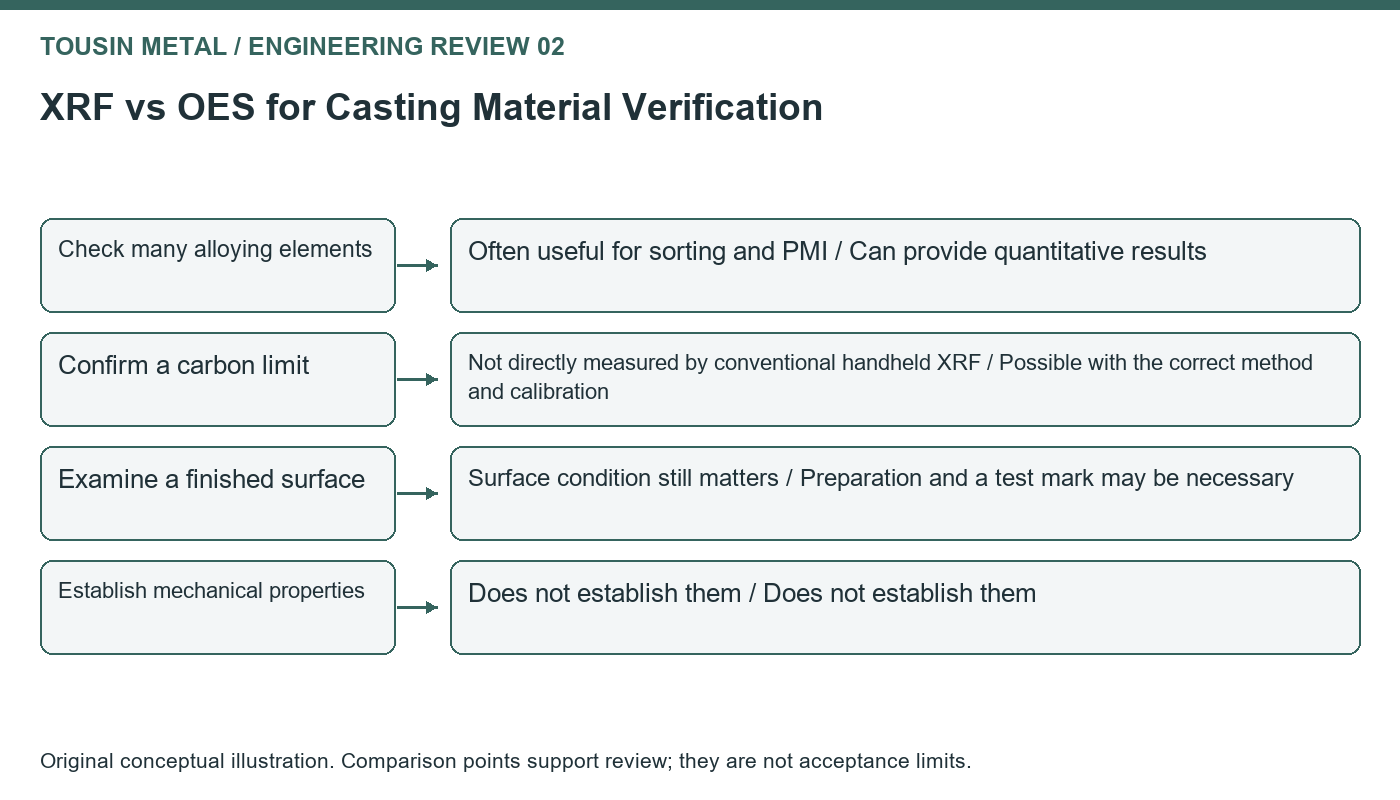
| Check many alloying elements | Often useful for sorting and PMI | Can provide quantitative results |
| Confirm a carbon limit | Not directly measured by conventional handheld XRF | Possible with the correct method and calibration |
| Examine a finished surface | Surface condition still matters | Preparation and a test mark may be necessary |
| Establish mechanical properties | Does not establish them | Does not establish them |
Neither route replaces tensile testing, heat-treatment records or other requirements specified for the component. A chemistry result should remain a chemistry result in the final dossier, without being described as proof of all material properties.
Decide where testing can leave a mark
Some analytical methods require surface preparation or produce a localized mark. A seal face, polished decorative area or thin edge may be an unsuitable location. The inspection plan should identify acceptable testing zones before the operator chooses the most convenient visible surface.
For a small casting with no suitable area, the foundry and buyer may need to agree a representative sample route. That agreement must preserve traceability and explain what the sample represents. Testing an unrelated piece of stock does not resolve the identity of the delivered casting simply because the nominal grade is the same.
Investigate a surprising reading systematically
A surface coating, contamination, geometry or poor preparation can complicate a result. When one casting appears to differ from its heat certificate, isolate it and verify the record linkage first. Repeat the test under controlled conditions using the appropriate method before deciding that the entire heat is incorrect.
Imagine two visually identical components from different alloy families entering the same machining area. A portable screening check may identify the mix-up efficiently. By contrast, two grades separated mainly by a carbon limit demand a method capable of resolving that difference. The verification method follows the risk, rather than the other way around.
Make the purchase requirement auditable
State the elements or grade distinction to be checked, the permitted method, inspection stage, sampling scope and required report. Specify how part identity connects to the certificate and how inconclusive results are handled. An instruction such as ‘100% PMI’ is incomplete if the intended acceptance decision remains undefined.
Tousin Metal enquiries should include any carbon-sensitive material requirements with the initial drawing. Agreeing the evidence early allows the supplier to plan testing without damaging finished surfaces or discovering at dispatch that the selected instrument cannot answer the customer’s question.
Further reading
Evident: Important Considerations When Using XRF for PMI explains instrument limitations relevant to alloy verification. SFSA: Standards and Specifications for Steel Castings is a starting point for identifying the applicable casting specification, which should be confirmed in its required edition.


